

Brass Socket Head Screws from a Custom Manufacturer
Shi Shi Tong manufactures drawing-based brass socket head screws for assemblies that specify a brass body and an internal hex drive. Head proportions, socket geometry, thread and seating dimensions are reviewed together for the complete part.
Identify the Head, Drive and Brass Body
A brass socket head cap screw combines a cylindrical head, an internal hex drive and an external machine thread. The hex key approaches along the screw axis, while the underside of the head bears against a flat seat or a suitable counterbore floor.
This page covers a brass-bodied screw. Brass-plated steel and steel screws with a brass tip have different constructions. A countersunk socket screw also needs a different head seat.
Illustrated Custom Configuration
The example below has an elongated cylindrical head and a short threaded stem. Its proportions are defined for this configuration rather than presented as a standard catalogue series.
| Feature | Illustrated value | Specification boundary |
|---|---|---|
| Threaded-stem diameter callout | 2.50 mm | The diameter callout does not establish the complete thread designation or pitch. |
| Stem-length callout | 4.10 mm | This is not a stated usable engagement length; the production drawing must define its measurement datum. |
| Cylindrical-head diameter | 4.00 mm | Check the surrounding clearance and any counterbore against the final drawing. |
| Cylindrical-head height | 4.70 mm | Include the head projection and the tool approach space in the assembly review. |
These values identify this example only. They are not a stock-size range or a tolerance statement. Thread pitch, socket dimensions, material grade and acceptance limits are defined separately for manufacture.
Explore other brass screw configurations
Fit the Head and Driver as Well as the Thread
A thread can fit while the screw still fails to seat or the tool cannot reach the socket. Check the complete installed envelope before choosing a catalogue description or copying a replacement part’s diameter.

Assembly Considerations:
- Hex-key approach
- Head clearance
- Bearing plane
- Under-head length
- Usable thread
- Thread runout
- Blind-hole clearance
| Selection point | What a compatible assembly needs | Common mismatch to avoid |
|---|---|---|
| Thread system and fit | The complete metric or inch designation, pitch or TPI, and the specified mating fit. | Similar measured diameters do not make metric and inch threads interchangeable. |
| Head diameter and height | Clearance for the cylindrical head, including any counterbore and installed projection. | A matching thread size does not guarantee a matching head envelope. |
| Hex socket | The specified across-flats size, recess depth and access for the correct hex key or bit. | An undersized or poorly seated tool can damage the recess. |
| Under-head length | A length measured from the defined bearing plane, matched to the clamped stack and available hole depth. | Counting the head in the working length or letting the stem bottom before the head seats. |
| Usable thread and runout | Enough complete thread in the mating part, with the runout and any plain section outside interference areas. | Treating every visible thread turn as effective engagement. |
| Bearing face | A suitable flat contact area with clearance around the under-head transition. | A sharp hole edge or unsuitable counterbore contacting the transition before the bearing face seats. |
| Finished condition | Thread and socket fit evaluated with the specified surface treatment and assembly condition. | Assessing only the unfinished part when a coating changes the functional dimensions. |
Brass needs an installation setting established for the actual alloy, screw geometry, mating thread and friction condition. A steel socket-screw torque table is not an installation setting for a brass replacement. Evaluate the required clamp load, recess condition and thread integrity in the intended assembly.
Choose Brass for a Defined Assembly Requirement
Brass is a copper-zinc alloy. Its material properties, appearance and response to the service environment depend on the selected alloy and condition. An internal hex drive is useful where an axial tool path is available and there is limited room for an external wrench around the head.
| Assembly requirement | Why this construction may fit | What determines suitability |
|---|---|---|
| A visible fixing that should match brass components | A brass body can provide material and appearance continuity through the part. | Alloy, finished appearance, handling marks and the acceptable change in colour during service. |
| An instrument or equipment assembly with restricted side access | The internal hex drive moves the tool interface into the cylindrical head. | Axial tool access, recess engagement, head clearance and the permitted tightening setting. |
| An electrical assembly that calls for a copper-alloy fastener | Brass can be considered where the specification requires a conductive metal fastener. | The complete current path, contact design, finish, heating and electrical validation of the assembly. |
| A replacement part with an unusual cylindrical-head proportion | Drawing-based manufacture allows the head, socket and stem to be reviewed as a defined geometry. | Functional dimensions, mating components, manufacturing feasibility and agreed acceptance criteria. |

Specify the alloy before the finish
H62 and H65 brass are material directions for drawing review. The selected grade and condition must suit the part geometry and manufacturing plan. An ASTM or EN designation should be evaluated against its exact requirements rather than treated as an automatic equivalent.
If plating is required, the substrate remains brass. Surface treatment, coating allowance, recess dimensions and thread fit need to be evaluated together. A brass-coloured coating on steel describes a different product.
Custom Manufacture Around the Complete Part
Head and socket geometry reviewed together
An elongated head, a restricted drive opening or a short threaded stem can change how a screw is made and assembled. Shi Shi Tong reviews those features on the same drawing, including the relationship between the recess, head wall, bearing surface and mating thread. The illustrated configuration is one example of a drawing-defined cylindrical head.
Material and finished fit in one specification
The brass grade, material condition and requested surface treatment are considered alongside the functional dimensions. This gives the manufacturing and inspection plan a defined part to work to, including the thread, drive and seating features that matter in the finished assembly.
Manufacturing and Inspection in Shenzhen
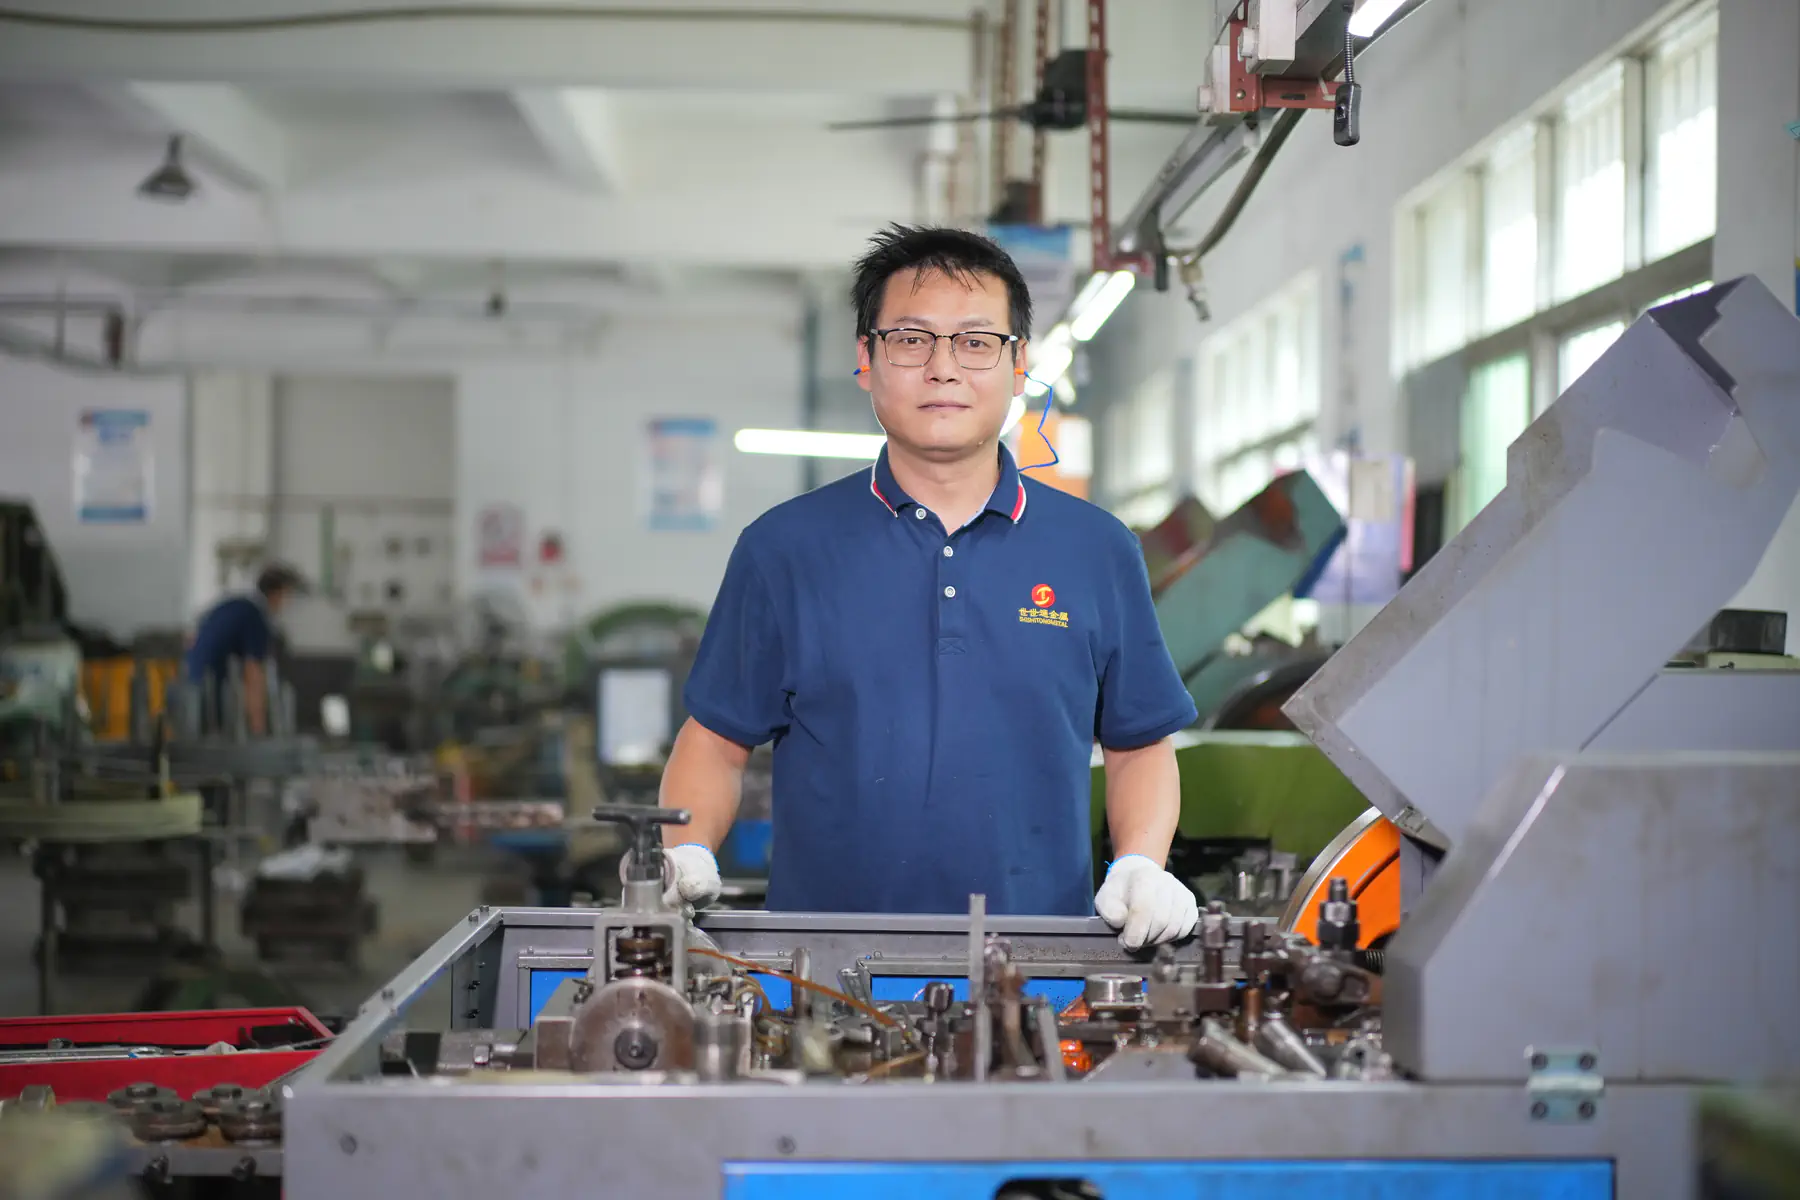
Shi Shi Tong has worked in screw manufacturing since 1998. Our Shenzhen operation reviews custom parts for material, geometry, manufacturing feasibility and the critical features that need to be controlled.
Inspection linked to functional features
Dimensional inspection, optical profile inspection and thread gauging support the inspection plan. For a brass socket head screw, the relevant checks can include the head envelope, recess geometry, thread and bearing dimensions. The exact methods and acceptance limits are established for the project.
Where torque, hardness, corrosion or other verification is required, the method, test conditions and acceptance criteria form part of the project review.


Brass Socket Head Screw Buying Guide
Compare the material, service environment and supplier requirements before approving a custom part for repeated purchase.
How do brass socket head screws compare with stainless steel versions?
Choose between brass and stainless steel by the complete material and assembly requirements. Neither name alone defines strength, corrosion performance or a safe tightening setting. A direct replacement needs the grade, condition, head, drive and thread to be checked together.
| Comparison | Brass version | Stainless steel version |
|---|---|---|
| Material identity | A specified copper-zinc alloy, with its material condition defined. | A specified stainless grade and condition; different stainless grades are not interchangeable. |
| Appearance | A brass-coloured body that may tarnish or develop a patina in service. | A different base-metal appearance; finish and environmental effects remain grade-dependent. |
| Electrical requirement | Can be considered for a conductive copper-alloy fastening specification. | Requires a separate review of the contact design and electrical performance; visual similarity is not an electrical equivalence. |
| Mechanical duty | Clamp load, recess strength and thread integrity must suit the chosen brass alloy and geometry. | Strength depends on the actual grade, condition and fastener specification. Recheck the joint before substituting materials. |
| Corrosion selection | Review the alloy, moisture, chemicals and contact with other metals. | Review the stainless grade against the same service conditions. |
For this custom brass product, H62 or H65 can be a starting point for material review. Keep the material designation on the drawing and assess any proposed alternative before changing the purchase specification.
Explore the broader brass screw rangeAre brass socket head screws suitable for outdoor equipment?
They may be suitable for an outdoor assembly when the alloy, exposure and mechanical duty have been evaluated. Brass can change colour or develop a surface patina; an appearance change and loss of structural function are different acceptance issues.
Persistent wetness, salts, chemicals and contact with dissimilar metals need particular review. Some conditions can cause dezincification, which selectively removes zinc from brass. A brass designation alone does not establish suitability for marine exposure, immersion or a specified service life.
Define whether the requirement concerns appearance, retained mechanical function or both. If testing is required, agree the exposure conditions, assembled materials and acceptance criteria for the part. Salt-spray hours alone do not establish outdoor years of service.
Review corrosion and salt-spray requirementsWhat should I verify when qualifying a manufacturer?
Start with the supplier’s ability to make and inspect the defined part. A similar product photograph helps identify the construction, but approval depends on the drawing revision, material requirement and functional checks agreed for your order.
- Material identity — establish the specified brass grade, condition and any required evidence of composition or restricted substances. A yellow appearance is not a material certificate.
- Functional geometry — identify the critical head dimensions, socket fit, thread and bearing features, then agree how each will be assessed.
- Sample approval — define the measurements and assembly checks that a sample must pass. Record any approved deviations against the drawing revision.
- Production control — agree the inspection scope, lot identification and records required for subsequent batches.
Shi Shi Tong reviews drawing feasibility and project-specific inspection requirements before defining the manufacturing plan. Requested material documentation, test reports and batch records should be named during quotation so that their exact scope can be established.
Review inspection methodsWhat should an RFQ define for bulk and repeat orders?
A comparable quotation needs one controlled part specification and a clear supply arrangement. A diameter, length and brass description alone can leave different suppliers pricing different head proportions, threads, finishes or inspection work.
| RFQ item | Why it affects the quotation or repeat order |
|---|---|
| Part number and drawing revision | Identifies the geometry and approved specification being priced. |
| Brass grade, condition and finish | Defines the material and finished state rather than an appearance-only description. |
| Complete thread and socket requirements | Establishes the mating fit and drive geometry. |
| Quantity per order and expected repeat demand | Provides a basis for assessing tooling, production planning and supply arrangements. |
| Sample, inspection and document requirements | Identifies the work and acceptance evidence included in the scope. |
| Packaging, lot identification and delivery destination | Defines handling, identification and logistics requirements for the order. |
For a Shi Shi Tong custom quotation, order quantity, tooling, sample requirements, documentation and schedule are established for the defined part. For repeat purchases, reference the approved revision and identify any change in material, finish, assembly or acceptance criteria.
Discuss Your Brass Socket Head Screw
Share a drawing or reference part together with the brass specification and order quantity. Include the mating thread, head clearance and any inspection or document requirements so the quotation can address the actual assembly.
