Custom Long Black Screws Manufacturer for Metal Assemblies
Shi Shi Tong manufactures made-to-drawing long black machine screws for equipment, enclosures, battery assemblies and other metal-component applications. Configure the head, drive, diameter, overall length, thread zone, material and black surface finish around your approved drawing.
- M1.4–M12 Diameter Range
- Lengths from 2–2000 mm, Subject to Review
- Manufacturing Experience Since 1998
- ISO 9001 Quality Management
Final feasibility depends on the complete geometry, material, tolerance, thread and finish requirements.
What We Mean by Long Black Screws
Long black screws are not defined by color alone. For an industrial project, the complete specification must identify the screw type, diameter, length measurement method, thread, material, mechanical requirements and black surface treatment.
Shi Shi Tong focuses on custom machine screws and special fasteners for metal and equipment assemblies. We do not position this page as a source for wood screws, drywall screws, anchors, expansion screws or self-drilling screws.
A black appearance does not automatically provide outdoor corrosion resistance. The substrate, pretreatment, coating system, thickness, assembly conditions and test method must be reviewed together.
Long Black Screw Types We Can Evaluate
Select a starting configuration, then send the drawing or critical dimensions for manufacturing and finish review.
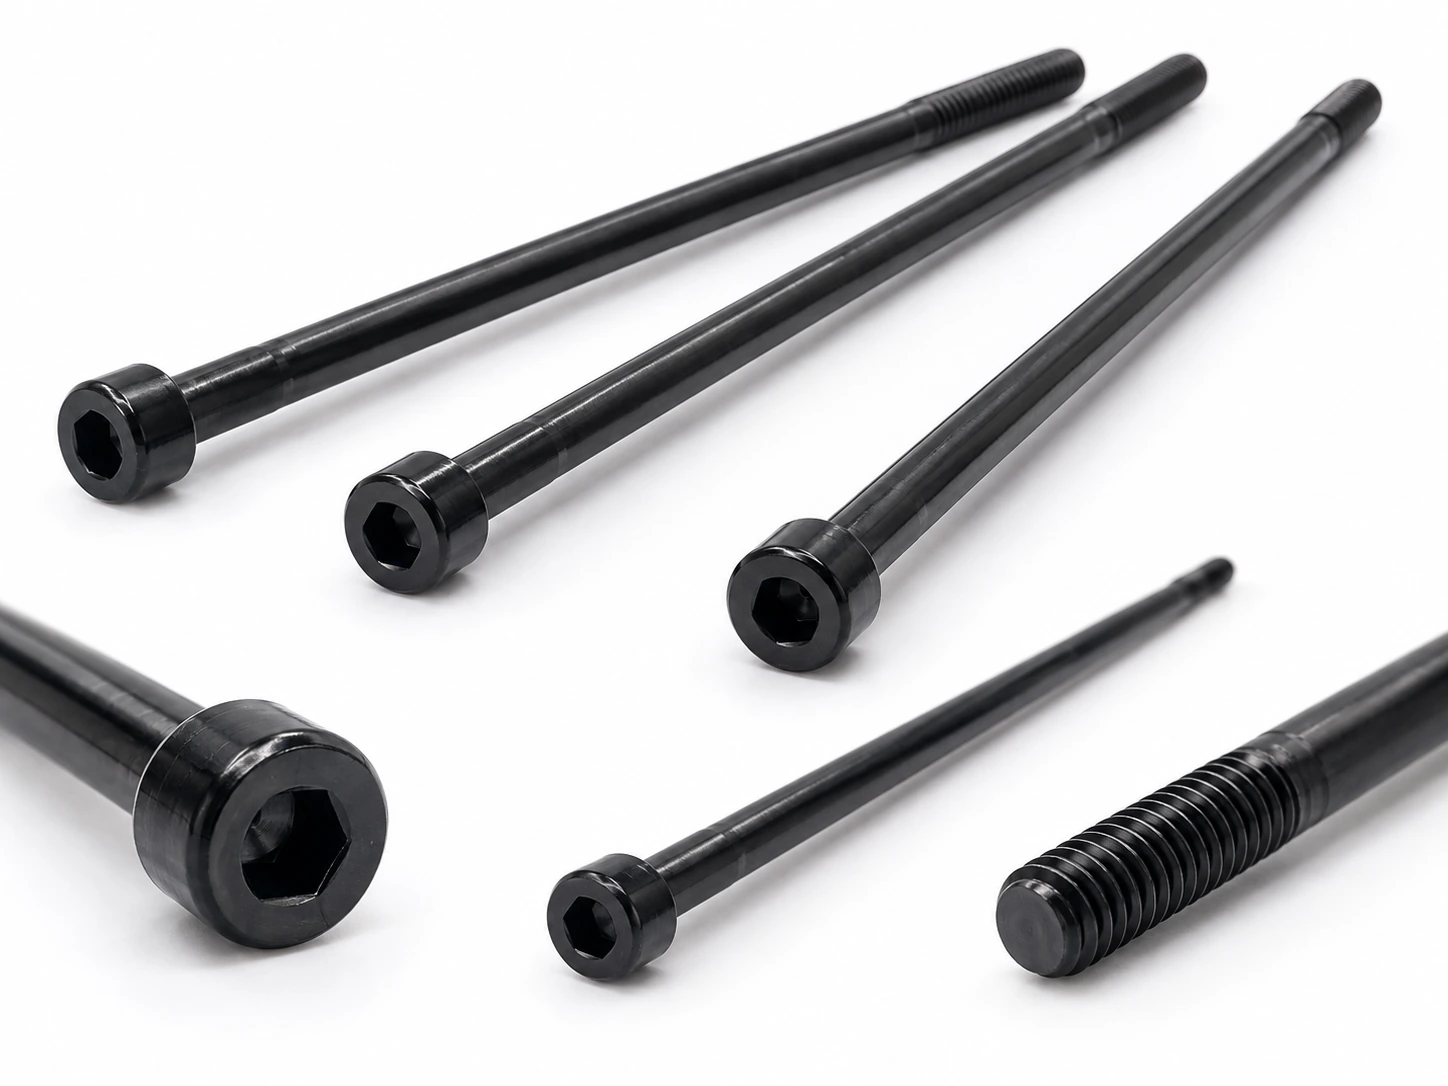
Long Black Socket Head Machine Screws
A practical starting point for recessed-drive assemblies that require controlled installation and a long reach. Available as fully or partially threaded configurations according to the drawing.
- • Hex socket and reviewed special-drive options
- • Full or partial thread
- • Carbon steel, alloy steel and selected stainless grades
- • Electrophoretic black, black oxide, black zinc and other reviewed finishes
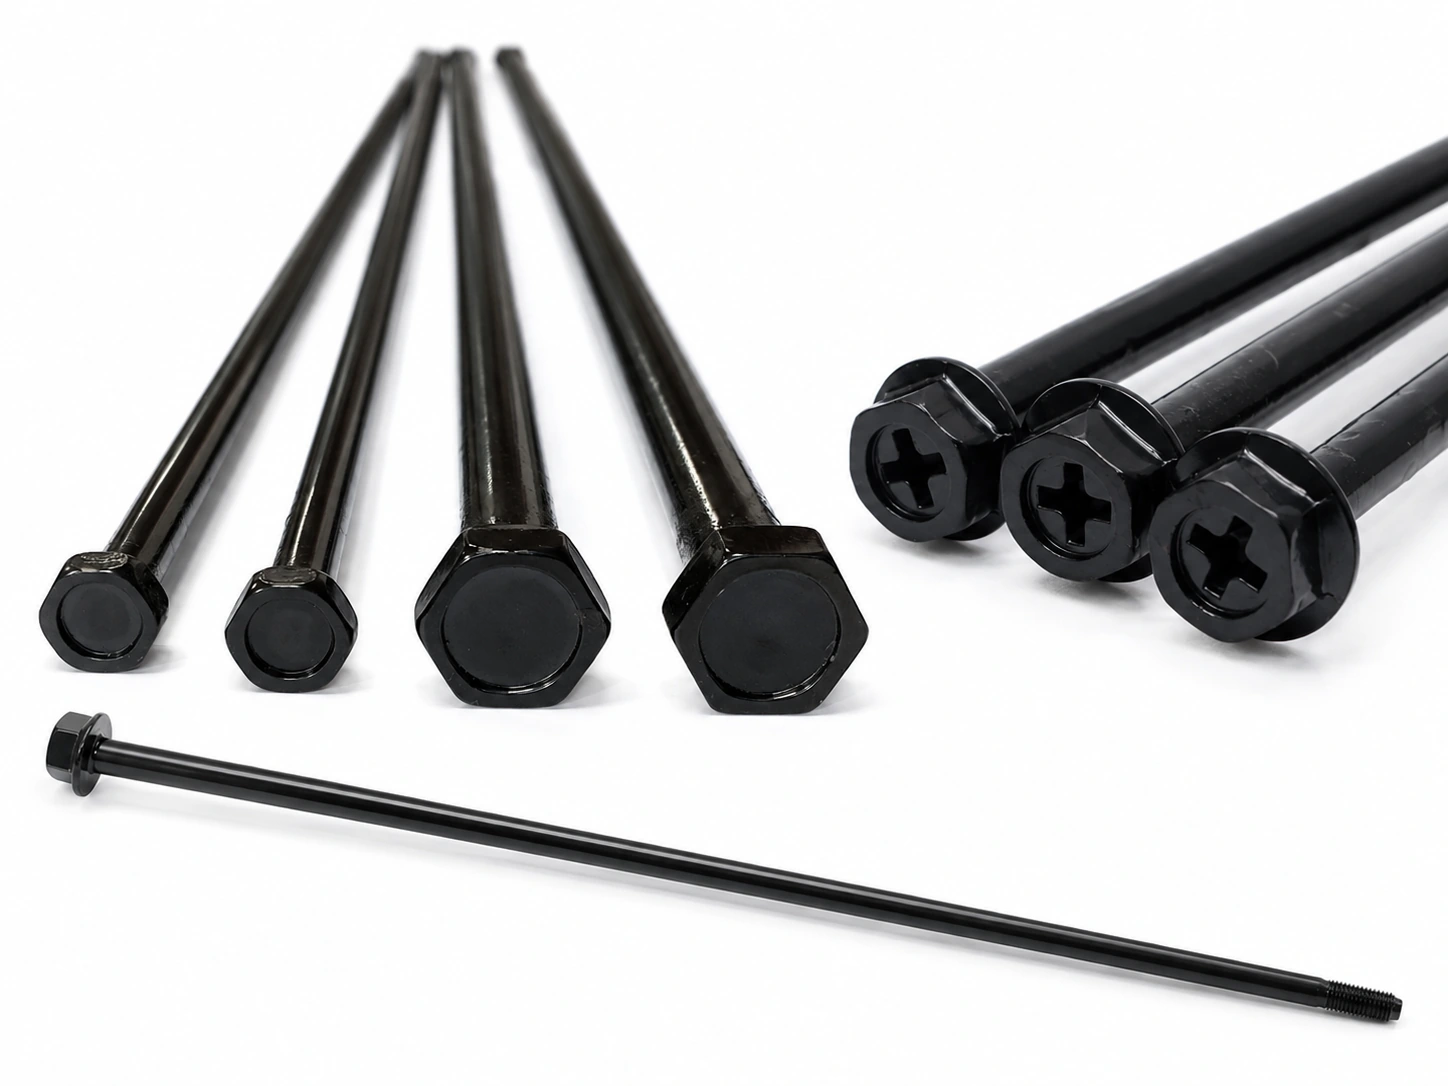
Long Black External Hex & Flange Head Screws
Designed for assemblies where external wrench access is available. Flange geometry, bearing surface and under-head details can be developed around the mating component.
- • External hex and hex flange configurations
- • Custom shank and thread-zone lengths
- • Optional washer-face or project-specific under-head geometry
- • Finish selected for material, fit and service conditions
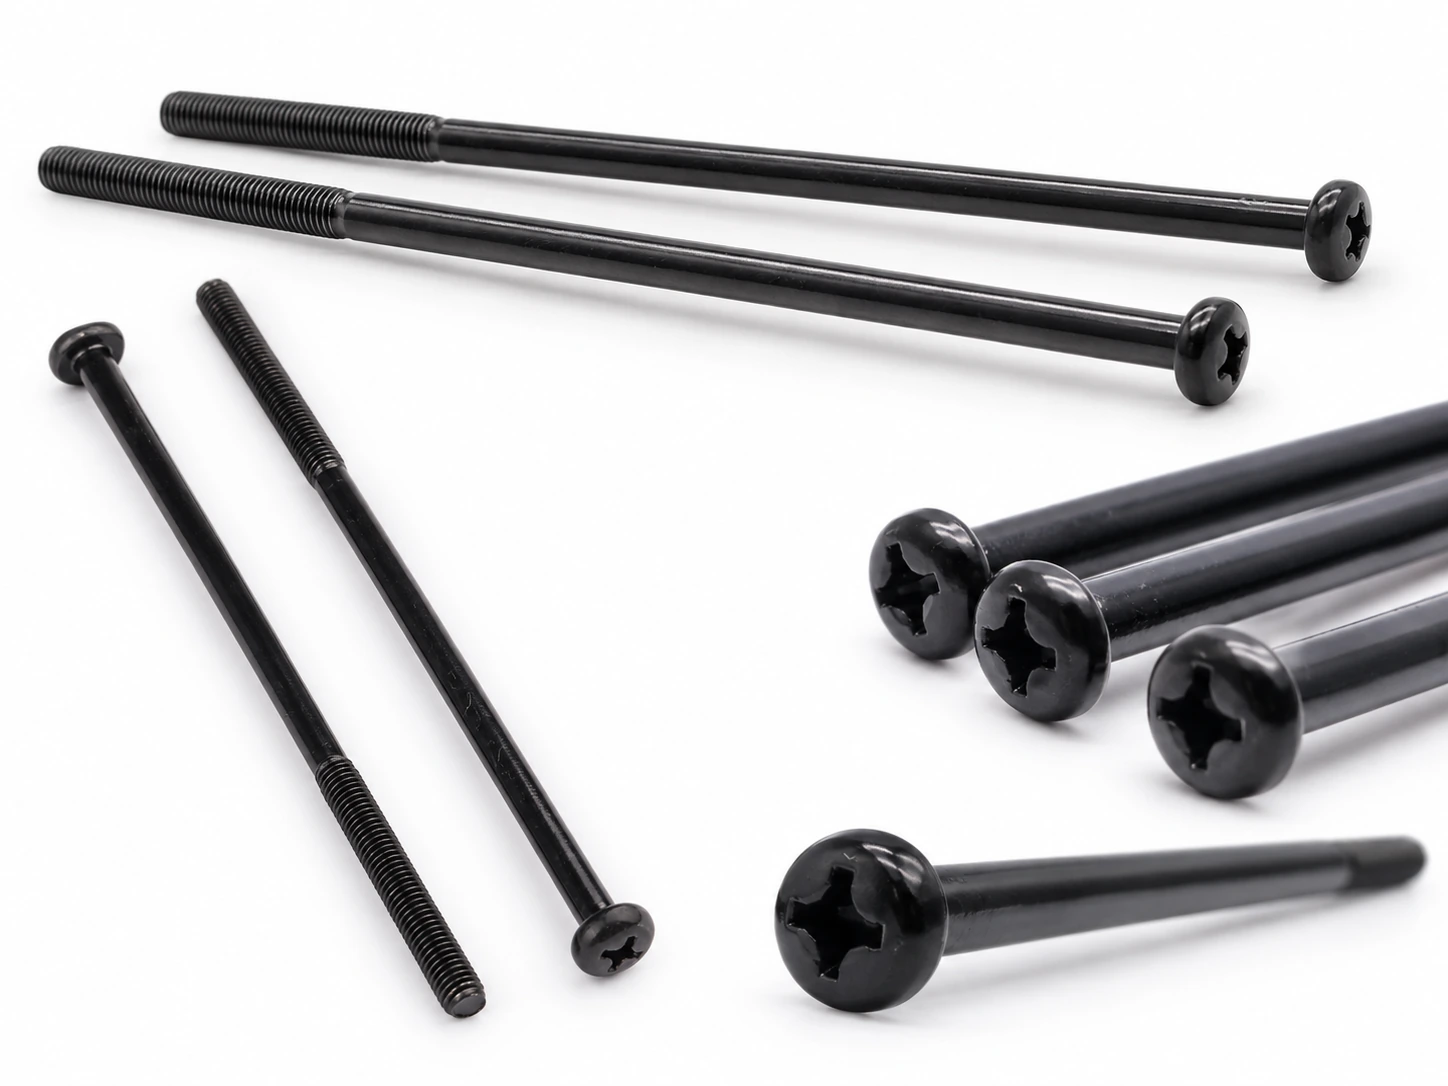
Long Black Phillips & Pan Head Machine Screws
Suitable for selected equipment, enclosure and component assemblies that require a cross recess and a defined visible head profile.
- • Phillips, pan and reviewed combination-drive designs
- • Custom diameter, length and thread coverage
- • Appearance sample approval where visual consistency matters
- • Coating allowance reviewed against recess and thread fit
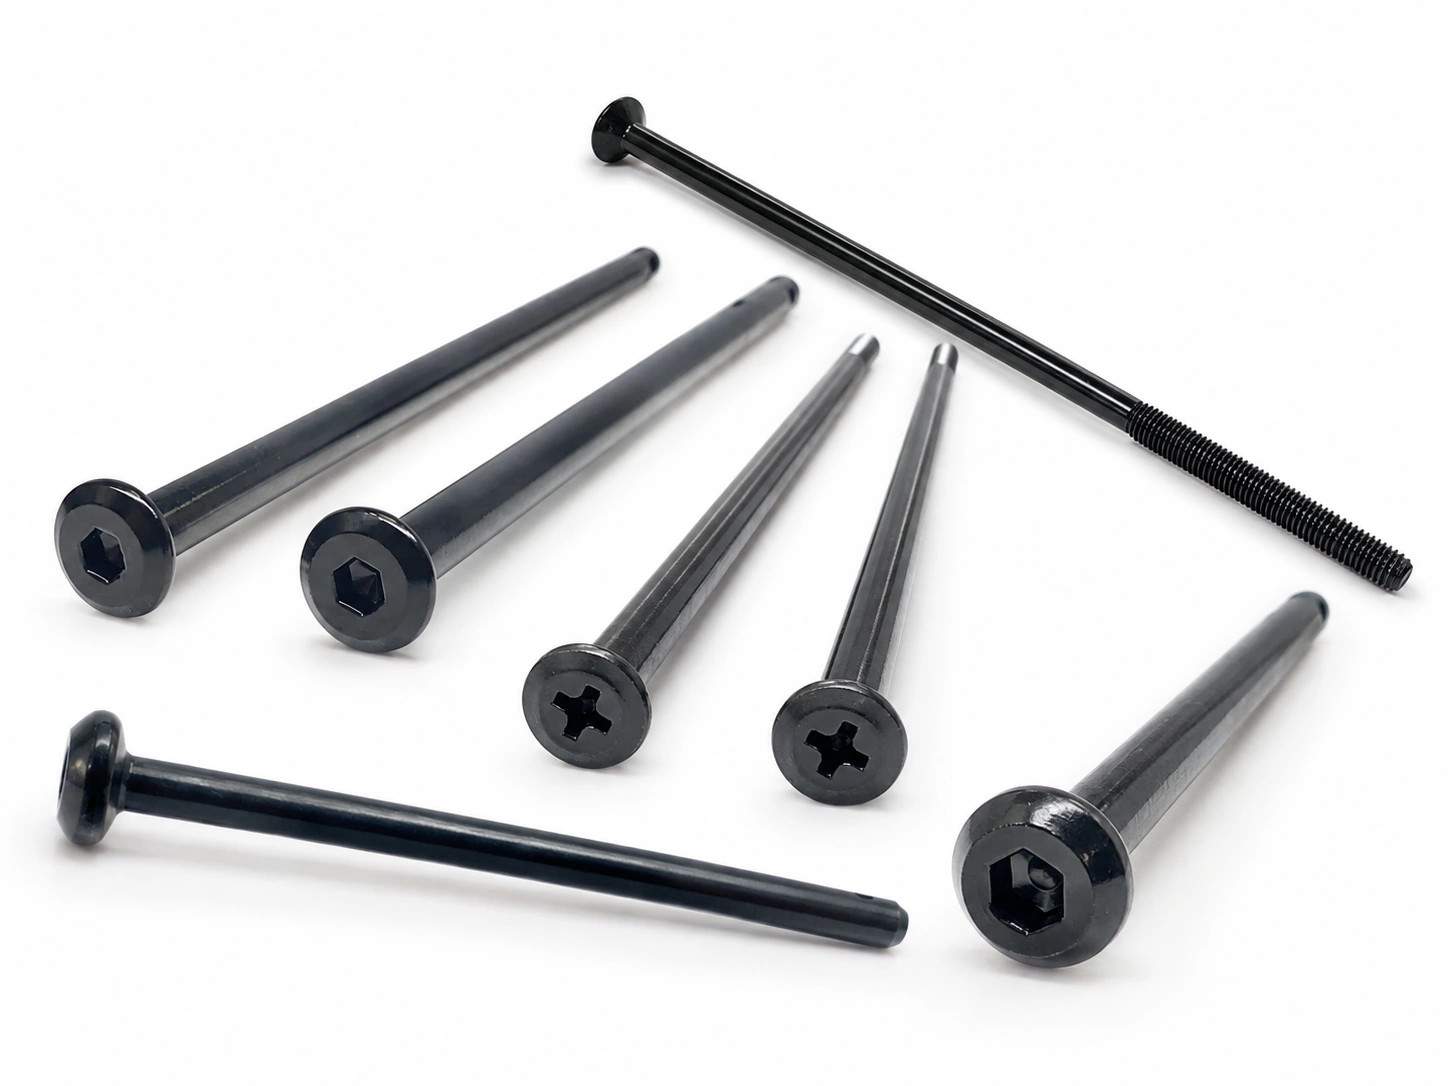
Custom Long Black Shoulder & Special-Geometry Screws
For projects requiring a shoulder, reduced section, knurl, step, special tip or another non-standard feature beyond a conventional machine screw.
- • Custom shoulder diameter and length
- • Stepped or reduced shank geometry
- • CNC secondary machining when required
- • Project-specific tolerance and inspection planning
Choose the Black Finish by Function, Not Color Alone
“Black” may describe several different surface-treatment systems. The correct route depends on the base material, target appearance, corrosion test, dimensional fit, hardness and assembly environment.
| Finish Route | Typical Project Fit | Items to Confirm |
|---|---|---|
| Electrophoretic Black Coating | Selected carbon-steel machine screws requiring a smooth black appearance and defined coating coverage. | Pretreatment, coating thickness, gloss or color sample, adhesion, abrasion exposure, recess clearance, thread fit and the required corrosion test. |
| Black Oxide / Blackening | Selected steel projects where a thin dark conversion finish is compatible with the application and approved protection system. | Base material, post-treatment oil or seal restrictions, storage and transport conditions, assembly environment and project-specific corrosion requirements. |
| Black Zinc Plating | Selected carbon-steel fasteners requiring a black plated appearance. | Plating specification, thickness, color sample, thread allowance, contact materials and hydrogen-embrittlement review for high-strength parts. |
| Black Zinc-Nickel Plating | Selected steel projects with a defined coating specification and corrosion-test requirement. | Coating system, thickness, topcoat, test method, failure criterion, thread fit and hydrogen-embrittlement controls where applicable. |
| High-Temperature Blackening | Selected stainless-steel or steel projects after material and process compatibility review. | Exact material grade, temperature effect, color expectations, dimensional requirements and corrosion-test specification. |
| QPQ | Selected components where the engineering drawing specifically requires a reviewed thermochemical treatment route. | Substrate, hardness requirements, dimensional effect, functional surfaces and post-treatment inspection. |
Define the Screw Before Requesting a Quote
A usable RFQ should describe more than the overall length. Long fasteners are sensitive to the relationship between head geometry, shank length, thread coverage, straightness, material and finish thickness.
| Parameter | Available Project Scope |
|---|---|
| Nominal Diameter | M1.4–M12, subject to geometry and process review |
| Length | 2–2000 mm, subject to diameter, material, geometry, tolerance and process review |
| Thread | Metric and other drawing-defined thread systems |
| Thread Coverage | Fully threaded, partially threaded or custom thread-zone length |
| Head Styles | Socket, external hex, flange, Phillips, pan and reviewed special heads |
| Shank | Plain, reduced, stepped, shoulder or drawing-defined |
| Materials | Carbon steel, alloy steel and selected stainless grades; other materials by review |
| Black Finish | Electrophoretic coating, black oxide, black zinc, black zinc-nickel and other compatible reviewed processes |
| Production Route | Single-die cold heading, multi-station forming, open-die forming for suitable long screws, thread rolling and CNC secondary machining |
| Inspection | Drawing-based dimensional, thread, hardness, material and project-specific inspection |
Countersunk and semi-countersunk screws are commonly measured including the head. Other head styles are commonly measured from below the head. The approved drawing or applicable standard takes precedence.
How to Choose the Correct Length for a Black Machine Screw
Measure the complete clamped stack, including brackets, covers, washers, spacers and gaps that remain after assembly.
Define the required thread engagement from the mating material, load, thread size and engineering standard. Do not rely on one universal engagement rule.
Confirm whether the specified length is measured from below the head or includes the head.
State the required thread length and the unthreaded shank length separately when a partial thread is needed.
Check clearance around the head and drive tool as well as the space available beyond the mating thread.
Review straightness, runout, handling and assembly access when the length-to-diameter ratio is high.
Include coating thickness and thread-fit requirements when a plated or coated black finish is specified.
If an existing screw must be reproduced, provide the drawing whenever possible. A physical sample can support review, but the drawing should define the acceptance requirements.
Common Risks in Long Black Screw Projects
A Black Finish Is Specified Without a Finish Standard
The same visual description can refer to different coating or conversion systems. We review the substrate, appearance sample, thickness, corrosion test and assembly environment before recommending a route.
The Screw Is Long but the Drawing Controls Only Overall Length
A long screw may also require control of thread-zone length, shank diameter, straightness, runout, head geometry and the transition between formed and machined features.
Coating Changes Thread or Drive Fit
Coating thickness can affect thread engagement, recess fit and under-head dimensions. These interfaces should be identified before sample production.
Outdoor Use Is Assumed from the Black Color
Color is not a service-life specification. Outdoor suitability must be evaluated from the base material, complete coating system, contact materials, exposure, test requirement and maintenance conditions.
Applications for Custom Long Black Machine Screws
The following are representative industrial applications, not universal approvals. Final suitability must be determined from the drawing and operating environment.
Battery and Energy-Storage Assemblies
Long-reach fastening for selected battery core packs, brackets and enclosure assemblies.
Machinery and Production Equipment
Custom lengths and thread zones for guards, frames, mechanisms and equipment components.
Automation and Positioning Equipment
Special shanks, shoulders or long-reach configurations for sensors, fixtures and positioning assemblies.
Metal Enclosures and Electronic Equipment
Black fasteners for selected panels, housings, mounting structures and visible metal-component assemblies.
Custom Fixtures and Structural Components
Drawing-defined fasteners for metal fixtures and assemblies where standard catalog dimensions do not fit.
A Manufacturing Route Built Around the Drawing
The production route is selected after reviewing the diameter, length, head, thread, material, tolerance and finish.
Drawing and Application Review
Confirm the geometry, measurement method, material, mechanical requirements, finish and inspection criteria.
Forming Route Selection
Evaluate single-die cold heading, multi-station forming or open-die forming for suitable long-screw geometries.
Thread and Secondary Features
Apply thread rolling and CNC secondary machining where the design requires shoulders, steps, reduced sections or special tips.
Black Finish Coordination
Match the treatment to the substrate, appearance target, dimensional interfaces and defined test requirements.
Inspection and Sample Validation
Inspect critical dimensions, threads and drawing-defined characteristics before production approval.
M6 × 272 mm Black Oxide Socket Head Screw for a Battery Pack Assembly
A U.S. battery-pack manufacturer required a one-piece long socket head screw instead of a welded construction. The approved configuration used an M6 × 1 thread, a 16 mm thread length, Property Class 8.8 carbon steel and a black oxide finish.
Shi Shi Tong developed the screw around the assembly requirements and produced samples for validation. After the samples passed the customer’s assembly validation, the project moved into batch production, including an approximately 1.49-metric-ton shipment.
- M6 × 272 mm overall configuration
- M6 × 1 thread
- 16 mm thread length
- Property Class 8.8 carbon steel
- Black oxide finish
- One-piece formed construction
- Battery core pack assembly
This case demonstrates a completed project, not a universal specification. New projects require an independent drawing, material, process and finish review.
Verification for Long, Coated and Special Fasteners
Long black screws must be evaluated as mechanical components, not only by appearance. Shi Shi Tong combines drawing-based process planning with inspection appropriate to the controlled characteristics of each project.
Dimensional Inspection
Critical diameter, length, thread-zone, depth, radius, angle, concentricity and drawing-defined geometry.
Thread Verification
GO/NO-GO gauges, pitch verification and project-specific thread checks before approval.
Material and Hardness Checks
Material verification together with Rockwell or Vickers hardness testing when required by the specification.
Optical Measurement
Non-contact or optical inspection for suitable profiles and dimensional features.
Functional Project Tests
Torque, assembly checks and other agreed tests where the drawing or quality plan requires them.
- Manufacturing roots since 1998
- More than 50 production machines
- More than 10 inspection devices
- ISO 9001 quality management
- Custom sampling and inspection planning based on the project
Bulk and Custom Supply Instead of Small-Pack Retail
Shi Shi Tong supplies made-to-drawing screws for custom and batch manufacturing projects. We are not positioned as a retailer of standard small packs.
For an efficient review, send the drawing or provide the diameter, length, head, drive, thread, material, black finish, tolerance, application, estimated quantity and required inspection or corrosion-test standard.
Long Black Screw FAQs
What are common applications for long black screws?
How do I choose the right size long black screw for metal?
How is the length of a long machine screw measured?
Which black finish is best for outdoor use?
Are corrosion-resistant long black screws available?
Can Shi Shi Tong supply long black screws in bulk?
Do you manufacture long black wood screws or drywall screws?
What diameters and lengths can be evaluated?
What information should I send for a quotation?
What is the MOQ and lead time?
Send Us Your Long Black Screw Drawing
Tell us how the screw fits into your assembly. Our team will review the geometry, forming route, thread, material, black finish, tolerance and inspection requirements before confirming the manufacturing approach.
For the fastest review, attach a drawing and identify the critical dimensions and finish specification.